-
Why there's no universal "best" cutting tool for emergency work
-
Scenario A: Standard material, stock on hand, timeline just got shorter
-
Scenario B: Standard material, no stock, tight deadline
-
Scenario C: Difficult material, no time to experiment
-
Scenario D: Design not finalized — prototype or modification work
-
How to figure out which scenario you're actually in
Why there's no universal "best" cutting tool for emergency work
I coordinate emergency tooling procurement for a precision machining shop. Over the past eight years, I've handled 200+ rush orders — same-day aerospace fixes, weekend automotive die corrections, you name it. And I'll tell you upfront: the tooling decision that saves one job will waste your budget on another.
What separates them isn't the tool itself. It's the scenario.
I sort every rush request into one of four buckets before I even open a catalog:
- A: Standard material, timeline pulled forward, stock already on your shelf
- B: Standard material, zero stock, need it this week
- C: Difficult material — Inconel, titanium, hardened tool steel — with no room for experimentation
- D: Design isn't locked yet. Prototype or modification work.
Here's how the total cost picture looks different in each one.
Scenario A: Standard material, stock on hand, timeline just got shorter
This is the least painful scenario. You've got the inserts, the cutters are sharp, and the only variable is scheduling.
The trap here is overreacting. When a deadline moves up, the instinct is to reach for the premium tool — the Sandvik Coromant product with the exotic coating, the one that costs 40% more per insert. Don't. If you're cutting 4140 steel at standard parameters, a general-purpose CVD-coated grade is fine.
I learned this the hard way in 2023. A regular client called on a Thursday afternoon needing a batch of hydraulic manifolds by Monday. Standard 4140, nothing exotic. I panicked and ordered top-tier inserts overnight — $1,200 extra with rush shipping. The job ran at the same surface speed we always use. Those premium inserts wore out on the same schedule as our shelf stock. I essentially paid $1,200 for a false sense of security.
What actually mattered? Confirming machine availability and raw material lead time. The tooling was never the bottleneck.
TCO takeaway: The cheapest tool is often the one already on your shelf. Emergency premiums belong on logistics, not cutting edges.
Scenario B: Standard material, no stock, tight deadline
Now we're in actual emergency territory. You need inserts, and you need them fast.
This is where I see shops make their most expensive mistake: comparing sticker prices on a catalog page. Let me give you a real example from last quarter.
We needed CNMG inserts for a rush order of 316 stainless components — about 300 pieces, two-week deadline. Quote one: $8.50 per insert from a discount supplier, 10-day lead time. Quote two: $11.20 per insert from a local distributor, next-day availability.
The math seems obvious, right? Save $2.70 per insert. Except: the discount supplier's "10-day lead time" turned into 12 days (happens all the time), and we'd burn two days of production waiting. At our shop rate, two days of idle machine time costs $3,400. We'd have saved maybe $405 on inserts and lost $3,400 in throughput. Not even close.
The local distributor also included setup support — their rep walked our operator through the correct grade selection for the specific 316 condition. Free technical guidance worth more than the price difference.
TCO takeaway: Add the cost of idle time before comparing quotes. A $400 savings that delays production by two days is a $3,000 loss.
One thing I'm honestly not sure about: why some distributors consistently beat their quoted lead times while others consistently miss. My best guess is it comes down to how they manage their own internal buffer stock. But I've been wrong about that before.
Scenario C: Difficult material, no time to experiment
Titanium, Inconel, hardened steel above 45 HRC — these materials don't forgive guesswork. And when the deadline is tight, you have zero room for trial runs.
According to ISO 513:2012, carbide inserts are classified into six application groups by material: P for steel, M for stainless, K for cast iron, N for non-ferrous, S for heat-resistant alloys like Inconel, and H for hardened materials. This classification exists because cutting Inconel with a P-grade insert is like using a wood chisel on steel — technically possible, practically disastrous.
The counterintuitive advice here: spend more, but spend it in the right place. Not on the tool itself — on application engineering.
Sandvik Coromant's technical reps, for example, will run your specific material grade and cutting parameters through their recommendation software before you commit to a $400 insert. That service doesn't cost extra, but you have to ask for it. Most shops don't.
I learned this after a painful miss. We had a rush job on 17-4 PH stainless, hardened condition. I assumed the insert we used for annealed 17-4 would work fine with adjusted speeds. Didn't verify. Turned out the hardness difference was enough to chip the cutting edge within 15 minutes. We went through four inserts and lost half a day before a Sandvik Coromant rep on a different project suggested we try a different grade entirely — one designed for hardened stainless. Solved the problem in one phone call.
TCO takeaway: Tooling engineering support is free from most major manufacturers. Use it before the deadline is too tight to recover from a bad guess.
Scenario D: Design not finalized — prototype or modification work
This scenario breaks the normal tooling rules because you might not need cutting tools at all.
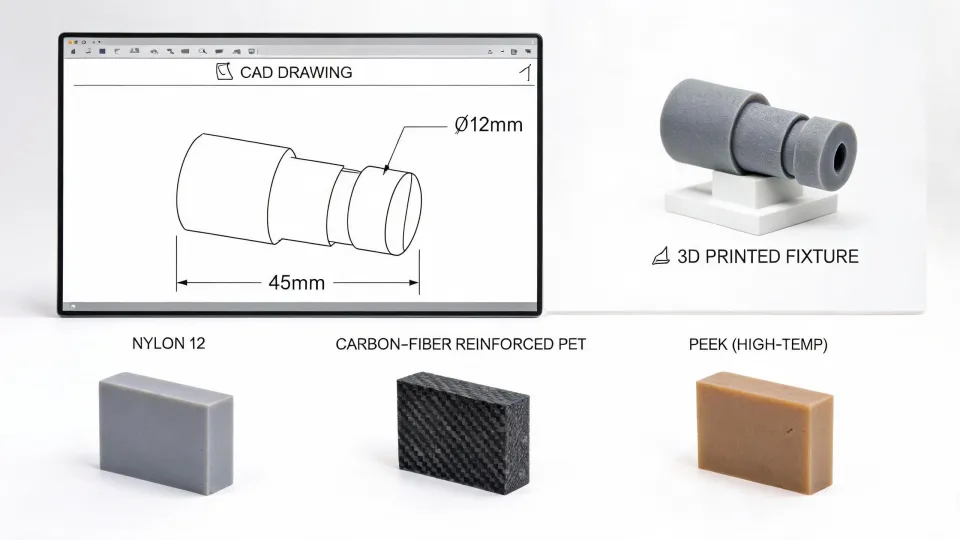
If the design is still shifting, or you're reworking an existing part, consider whether additive or welding processes can get you to "close enough" faster than CNC machining.
For form-and-fit checks, the current crop of affordable 3D printers for beginners in 2025 is genuinely useful — sub-$400 units that print dimensionally accurate PLA prototypes in a few hours. You're not committing to a carbide grade and a full CAM program just to hold a physical part in your hand.
Similarly, if you're modifying existing tooling or building quick fixture extensions, a portable laser welding machine can save days versus ordering custom components. I've reviewed a few sub-$1,000 units for our shop's repair bench; for light-duty work on steel and stainless, they're surprisingly capable, though duty cycle matters more than the spec sheet suggests.
One question I get from mold shops: can resin 3D printers print in color? Not in any way that matters for functional testing — resin color is cosmetic, and print resolution beats color accuracy every time for form-and-fit. But if you're using printed parts for client presentations before the final machined version, color helps avoid eyebrow-raises.
TCO takeaway: The cheapest tooling solution is sometimes not a cutting tool. A $300 prototype that reveals a design flaw is cheaper than a $3,000 machined part that has to be scrapped.
How to figure out which scenario you're actually in
Here's the uncomfortable truth: most shops misclassify their scenario, usually by skipping straight to Scenario C (buy the premium tool, order it overnight) when they're really in Scenario A or B.
Ask yourself these questions in order:
- Do I have the right tool on the shelf right now? If yes, you're in Scenario A. Use it. Don't overthink.
- Is the design final and the material standard? If yes, you're in Scenario B. Price the total delivered cost, not the unit cost.
- Is the material one of the "hard" families — titanium, Inconel, hardened steel, or any nickel-based alloy? If yes, you're in Scenario C. Call the manufacturer's technical line before you order anything.
- Could you deliver a functional but non-final part within 48 hours using a non-machining process? If yes, you're in Scenario D. Look at additive or welding options before committing to CNC.
I've never fully understood why more shops don't ask these questions before every rush job. The pressure of a deadline makes people skip straight to "buy the expensive thing and overnight it." That works sometimes. It wastes money almost every time.
Take it from someone who's still paying off the mistakes that assumption caused. The tool matters less than the scenario. Figure out the scenario first. The right Sandvik Coromant cutting tool — or the right alternative process — almost always becomes obvious after that.