For the past four years, I've handled purchasing for an engineering-led company of roughly 100 employees across three locations. I'm not an engineer. I'm the person who translates their requests into purchase orders. One thing I've learned is that the phrase Ultimaker 3D printer filament is not a complete order.
Neither is a phrase like 4 flute square end mill. Both need a machine context, a material spec, and an application before price makes sense. This guide covers the three buying scenarios I see most often, and how I decide which advice applies.
Start with the machine situation, not the brand name
The same product can be a good buy in one context and a costly mistake in another. Most of the buying mistakes I've made happened because I treated these contexts as one generic purchase. Here are the main scenarios:
- Scenario A: The printer is already in the building and you need material that works without turning every print into a research project.
- Scenario B: You are choosing a printer and its material ecosystem for the next few years.
- Scenario C: You buy for a mixed workshop, where requests include both 3D printing filament and cutting tools.
Scenario A: You already have a 2.85 mm printer
When a printer is already installed, the buying question isn't which filament brand is best. It's whether the material matches the machine and the part requirements.
What 3D printers use 2.85 mm filament?
From the orders I've handled, the Ultimaker S-line printers I see most often are the S3, S5, and S7. Those are 2.85 mm machines. The older Ultimaker 2+ line is also in that group. Most consumer-focused printers I've seen use 1.75 mm, so the word Ultimaker alone is not enough. Before I order, I check the official spec page. If the spec sheet doesn't say 2.85 mm or list a compatible material, I don't trust the product title. I want to say this sounds obvious, but product listings often call a filament universal when it isn't right for the profile you need.
Dealing with an ultimaker download request
There is also the software side. A request for ultimaker download usually means Cura, Ultimaker's slicer. For an S-line printer, Cura has material profiles that set temperatures and print speeds. I use the official Ultimaker download page for company installs. A file from a random forum can be outdated or unsafe, and outdated profiles create failures that look like material problems.
Ordering filament that actually works
After confirming the diameter and the software profile, I still don't order a full case by default. The order that taught me this was 40 spools of a discounted 2.85 mm PLA. The nominal size was right, but the diameter tolerance from spool to spool was poor. A printer that ran one roll cleanly would jam or under-extrude with the next. I still kick myself when I see the unopened boxes in storage.
Now I buy one spool, print a simple test piece, and compare the settings to the Cura profile. If a supplier can't provide a datasheet and the material has no profile, the risk goes up. That doesn't mean every generic filament is bad. It means the burden of proof is on the supplier.
The machine doesn't care what the label says. It cares what is coming out of the nozzle.
Scenario B: You are choosing a printer and material ecosystem
If no printer exists yet, don't start with a search for what 3D printers use 2.85 mm filament. Start with the parts your team needs to produce. In our 2024 vendor consolidation project, I compared build volume and hardware price first. I should have compared materials first.
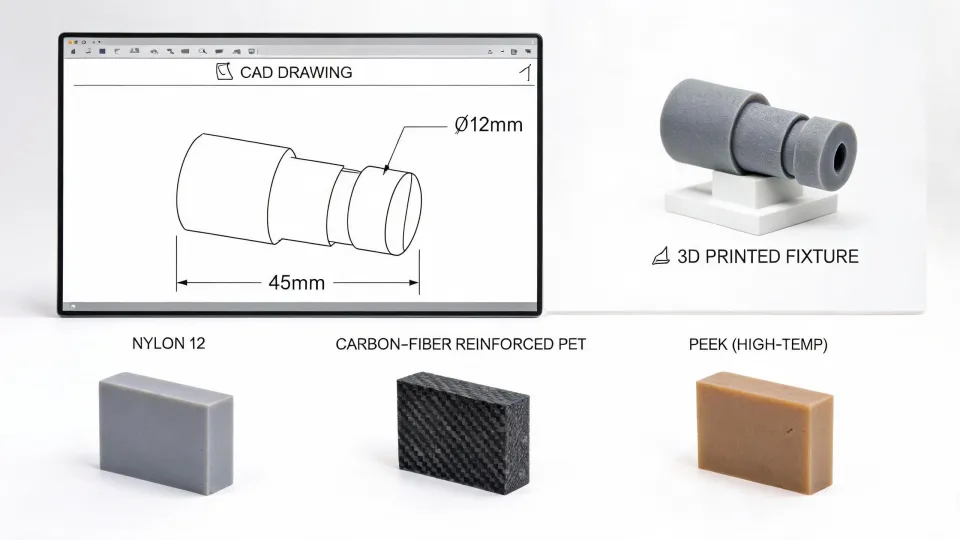
If the work needs engineering materials like polycarbonate, nylon, or PVA supports, the printer ecosystem matters more than the diameter number. A 2.85 mm machine with tested material profiles can cost more up front, but it can reduce failed prints and troubleshooting time. If the team only needs PLA prototypes, a simpler and cheaper route may be fine.
I also count training and support as part of the price. If every office uses a different machine and different slicer settings, support questions multiply. The total cost per good part is the only honest number I've found.
Scenario C: When 3D printing and CNC requests land on the same desk
This is where the earlier phrases come together. Buyers like me handle additive and subtractive processes in the same day. One morning I had to vet a wholesale square end mill manufacturer and get pricing on a 4 flute square end mill. The next request was for Ultimaker 3D printer filament for an S5. Those requests are different in almost every way, but they use the same sourcing rule: don't compare price before the spec is confirmed.
For the end mill, I don't decide the flute count on my own. A 4 flute square end mill can be a good choice for finishing, while a 2 flute tool often clears chips better in softer materials. I ask the machinist which geometry, coating, and brand they already use. If a wholesale square end mill manufacturer can't provide a cutting data sheet, I don't put them on the approved vendor list.
The filament order gets the same treatment. If the supplier can't provide diameter tolerance and a material profile that works in Cura, I don't order 50 spools. I order one sample and run it.
The processes are different, but the discipline isn't.
How to tell which scenario you are in
Instead of saying it depends, here is a quick test for your next request:
- If a machine is already on your floor, you are in Scenario A. Buy one test spool first unless the exact material has a proven history in that machine.
- If you are choosing the first machine or standardizing a lab, you are in Scenario B. Define the materials and required part properties before comparing models.
- If requests come from both 3D printing and CNC, you are in Scenario C. Keep separate approved lists for filament and cutting tools, and demand documentation in both.
I can only speak to my context: a mid-size product development team with a trained operator and roughly 200 orders per year. If you're in high-volume manufacturing, your process will be more formal. If you're in a school, it may be simpler. The spec-first habit still applies.
When in doubt, order one item instead of a case. Ask for a datasheet. Run one test. It takes a little longer, but it's how I avoid buying 40 spools of a problem I'll be looking at for years.