-
The comparison framework I use
-
Dimension 1: Time to first usable part
-
Dimension 2: What Ultimaker 2 3D printer specs do and don't tell you
-
Controlled environment for laser welding and facility requirements
-
Dimension 4: Real cost of an emergency order
-
The question nobody wants to hear: what do you actually need?
-
Which one should you pick?
I coordinate rapid-turn manufacturing for engineering clients, and I've handled more than 200 rush orders over the past few years. Last quarter alone, we processed 47 rush orders with 95 percent on-time delivery. Not perfect. But those jobs taught me to ask three questions first: how many hours are left, can this part physically be made in that time, and what happens if we miss?
The comparison I hear most often now is whether a 3D printer Ultimaker is a CO2 laser alternative. It's actually a fair question. Both can move small-batch production quickly, and both get pitched as fast-turn solutions. But they are not interchangeable. Here's how I compare them when a real deadline is on the line.
The comparison framework I use
I'm not comparing brands, and I'm not saying one machine is better in every job. I'm comparing two manufacturing methods: additive FDM on an Ultimaker and cut or engrave operations on a CO2 laser. Those methods create different lead times, geometry limits, facility requirements, and hidden costs. Those four dimensions decide the rush order.
Dimension 1: Time to first usable part
If you only look at cycle time, the laser often wins. A CO2 laser can cut flat parts in minutes. But a rush part isn't useful until it's installed or shipped. That's where a 3D printer can flip the math. A single FDM build can produce an entire bracket with bosses, snap fits, cable channels, and holes. A laser starts with flat sheet, so every 3D feature needs another step.
This is the setup trap. A 15-minute laser cut plus 90 minutes of hand assembly is slower than a 90-minute print that comes off the bed ready to test. If the file is already prepared in Cura and queued in Digital Factory, the printer setup is minutes, not hours. That doesn't make the laser bad. It just means the comparison should cover the entire workflow, not the cut time.
Bottom line: when the part is flat and ready to cut, laser wins. When the part needs real 3D geometry, the print wins because it removes secondary operations.
Dimension 2: What Ultimaker 2 3D printer specs do and don't tell you
Let's address the spec sheet. According to Ultimaker's published specs, the Ultimaker 2 3D printer specs include a 223 x 223 x 205 mm build volume, a standard 0.4 mm nozzle, and a minimum layer height of 20 microns. That was accurate as of the product generation I used. The market changes fast, so verify current specs and product availability on ultimaker.com before buying.
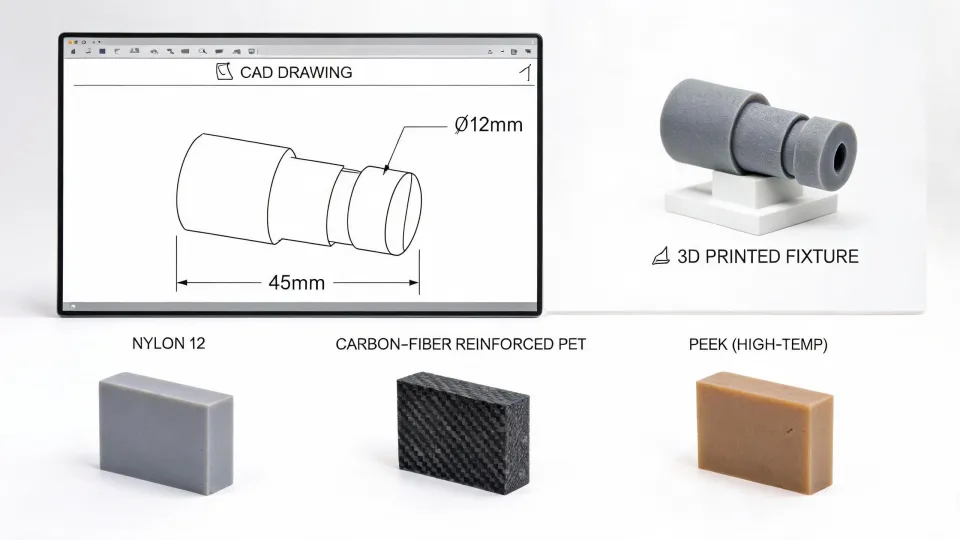
In a rush job, I do not run 20 microns. I run 0.2 mm layers and design for a 0.4 mm nozzle because that setup is repeatable. The spec that matters more is geometry. An FDM printer can make internal channels, undercuts, and enclosed housings in one go. A laser can't. It can only work with profiles that are visible from the beam direction.
The counterintuitive conclusion here is that dimensional accuracy isn't the main deciding factor. A super-clean flat cut still loses when it needs multiple secondary operations to become a usable part. A one-piece print with slightly lower resolution can save the deadline because you don't have to orient, fixture, and assemble it later.
Controlled environment for laser welding and facility requirements
This is where many emergency comparisons fall apart. A CO2 laser is not a self-contained process for every material. Cutting and engraving require fume extraction and often compressed air. If the application moves into laser welding, you need a controlled environment for laser welding: clean shielding gas, stable humidity, clean optics, and a properly rated enclosure. Nobody should pretend that can be set up in one afternoon.
An FDM printer is not zero-work, but its baseline is lower. Filament must be dry, and engineering materials often need an enclosed heated chamber. Still, an Ultimaker in a temperature-controlled production space can handle most polymer rush parts without gas bottles or a laser-safe room. If you don't already have the laser infrastructure, that facility requirement alone can be a deal-breaker.
To be clear, I'm not saying a 3D printer replaces laser welding. That would be wrong. For metal parts, follow the welding equipment manufacturer's environment specifications. But for a polymer part that needs to ship tomorrow, this dimension usually points toward the printer.
Dimension 4: Real cost of an emergency order
Unit price is the last number I trust. I still remember a rush project where we saved $35 by choosing a lower-priced laser vendor. The material wasn't stocked, so we paid $180 for freight. Then the first run failed because the machine wasn't calibrated. The re-run cost another $210. We saved $35 and ended up spending hundreds more than the in-house printed part would have cost.
I've also made the opposite mistake and 3D printed parts that should have been laser-cut. Flat polycarbonate panels, for example, are usually cheaper and faster on a laser when the sheet is available. So the goal isn't to defend one technology. The goal is to reduce process steps, risk, and wasted hours.
The question nobody wants to hear: what do you actually need?
This is the area where I've been burned more than any machine. I once read an email that asked, 'who makes VMC drinks?' In my world, VMC means vertical machining center, so I assumed a beverage company needed a CNC fixture. What made it worse is that I still don't know who makes VMC drinks. The real lesson was that we were using the same words but meaning different things. That confusion cost time, not money, and it is exactly the risk in any laser-versus-printer debate.
I hear 'CO2 laser alternative' and need to know: alternative for what? Are you cutting acrylic sheet, engraving anodized aluminum, or making a 3D part? Those are different jobs. A phrase like '3D printer Ultimaker' doesn't tell me whether you need a one-off part or 200 flat pieces. So I have adopted a policy: if an emergency order has any ambiguity, I reply with one-line confirmation before starting. It adds ten minutes and saves days.
Which one should you pick?
Use a CO2 laser alternative when the part is flat, the material is on site, and the geometry can be completed with 2D cuts. It's often the fastest route for acrylic, wood, and thin sheet stock. Use a 3D printer Ultimaker when you need internal geometry, design changes, or a complete part without secondary operations. When the deadline is tight, reducing variables is sometimes more important than reducing raw cut time.
Price per unit is not the only decision factor. Ultimaker earns its place through dependable repeatability and a smooth digital workflow, not through being the lowest-cost box in the catalog. And no 3D printer can replace all traditional manufacturing. Verify current specs with the manufacturer, check your facility safety requirements, and confirm the definition of the part before the clock starts.