On a Tuesday afternoon, I learned that the replacement bracket for a packaging line would take five business days. The line was supposed to start again in 36 hours. That is the moment this comparison is meant for.
I coordinate rapid fabrication for an industrial automation company, and I've handled 300+ rushed production jobs in 11 years—including same-day fixes for clients who measured delays in thousands of dollars per hour. When I'm triaging a rush order, I ask three questions first: what material is truly required, how many hours are left, and what does missing the deadline cost? Then I compare routes.
The two routes I see people weigh are printing an urgent part on an Ultimaker S5 R2 3D printer and sending it to a machine shop that will use the appropriate end mill milling cutter or carbide insert for turning. This is not an abstract technology debate. It's a comparison for the specific situation where 'by Tuesday' is the only detail that matters.
Dimension 1: Lead Time, Not Cycle Time
A machined part can be cut in 20 minutes. If the machine is free and the operator is ready, that route can be unbeatable. But a machine shop's backlog may be three days before your tiny job sees a spindle. The first number that matters is available hours, not machining minutes.
In March 2024, a customer needed a custom sensor bracket for an assembly line restart that same day. The shop next to our facility quoted a four-day lead. We had an Ultimaker S5 R2 3D printer running in the corner. I sliced the bracket in Cura, sent it to the printer through Digital Factory, and had a usable PETG part in under four hours. The metal version was ordered later; the line did not wait.
Before you jump to the objection: yes, the printed part was not as strong as aluminum. It didn't need to be. It was a sensor mount, not a lifting lug. Matching material to the actual function is part of the job.
Dimension 2: Setup, Tooling, and the Forgotten Consumables
If the route is CNC machining, the cutter is not an afterthought. Machining a pocket in aluminum requires an end mill milling cutter with the right diameter and coating. Turning the same component on a lathe means choosing a carbide insert for turning with the correct chipbreaker and radius. As of January 2025, I've seen reasonable tool prices at supply houses—an end mill milling cutter around $35 to $80, and a carbide insert for turning often between $12 and $25. Those numbers are manageable. The problem is discovering you need a different one after the machine has stopped.
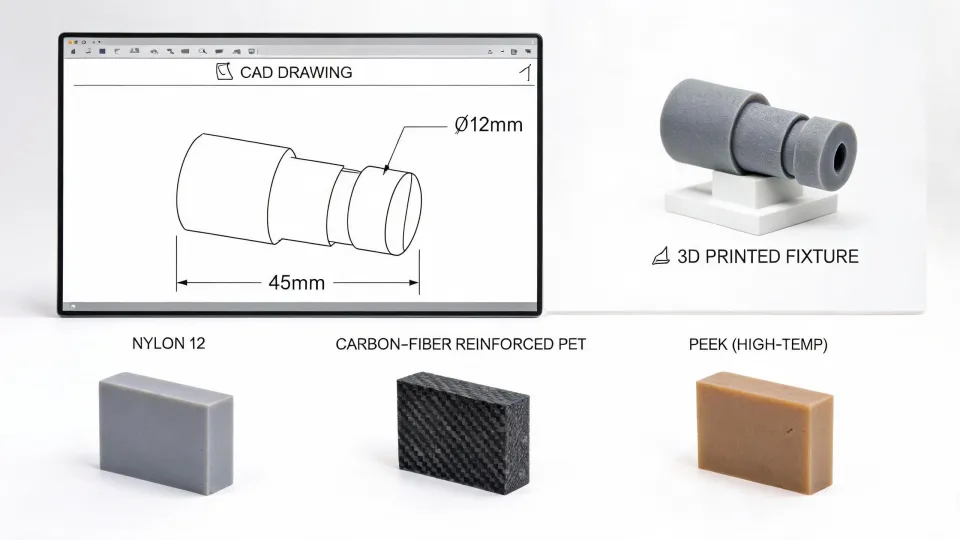
On an FDM printer, the equivalent setup is a Cura profile, a clean build plate, and a spool of material that hasn't absorbed moisture. There's no spindle speed to set, no coolant concentration to check, no worn insert to inspect. I'm not saying 3D printing is easier in every way. I'm saying that, for a one-off emergency part, the preparation time is lower and usually more predictable.
Dimension 3: Price the Worst Outcome, Not the Quote
I have mixed feelings about rush premiums. On one hand, they often feel like a penalty for someone else's scheduling problem. On the other hand, I've seen how an unscheduled job can wreck a machine shop's plan, so I understand why the premium exists. Under a real deadline, though, I don't compare the base price. I compare the expected cost of being late.
The example I always come back to happened in 2023. One vendor quoted $400 to machine a bearing housing, with delivery 'probably by Friday.' Another vendor quoted $750 with delivery Thursday, and wrote the time on the work order. The upside of the cheaper option was $350 in savings. The risk was that 'probably' would become 'next Tuesday' and our client's test would be pushed back two weeks. I kept asking myself: is $350 worth that risk? It wasn't. We took the $750 quote. The part arrived on Thursday morning.
You're not paying extra for a faster machine. You're paying to remove the word 'probably' from the delivery plan.
This is why I now tell engineers to add a 48-hour buffer when the deadline is not negotiable. It feels wasteful when nothing goes wrong. It feels cheap when everything else is on fire.
Dimension 4: Design Revision Risk—The Surprising One
I grew up in manufacturing hearing that 3D printing was for prototypes and CNC was for real production. The conventional wisdom is not wrong in every case. But for urgent little parts, the biggest risk is often a design error, not a material weakness.
Last year, we had a bracket where the original hole pattern was wrong. On a CNC route, fixing that means another block of aluminum, another setup, maybe another end mill milling cutter, and another entry in the shop's queue. On the Ultimaker S5 R2 3D printer, we edited the CAD file, re-sliced, and started a new print. The second plastic part was ready the next morning. That flexibility matters when the only way to get the design right is to test it against the actual machine it belongs to.
Everything I'd read said FDM parts would be the weak point in an emergency. In practice, the weak point is usually the wait between attempts.
A Quick Note on Other Digital Tools
I should add one side point, because many shops in this situation ask about lasers too. A common question is: can fiber laser engrave wood? It can, but the result is often charred and uneven, especially with soft woods. Fiber lasers are better suited for metals; if you need clean wood engraving, a CO2 laser or a router is the more predictable tool. The broader lesson carries over to the main decision: don't buy one tool because it sounds flexible. Match the tool to the deadline and the material.
So Which Route Do I Choose?
If the part can be made from thermoplastic, the geometry fits inside the build volume, and the hours are short, an Ultimaker S5 R2 3D printer is often the lowest-risk option. That's not because printing is superior; it's because holding a spool of filament in your hand beats waiting for a machine that is currently cutting someone else's job.
- Print it when the material requirement is within FDM limits, the design might still change, quantity is low, and the lead time is under two days.
- Machine it when the part must be metal, sees high heat or structural load, tolerances are tight, or the design is already frozen and volume is too high for layer-by-layer manufacturing.
- Use a laser for marking and engraving—not for making structural parts. And if the material is wood, choose the laser wavelength with care.
I've seen too many companies buy one capability and try to make every job fit. Some parts simply require an end mill milling cutter, a carbide insert for turning, and a skilled machinist. Other parts require a present printer, a calibrated Cura profile, and the nerve to start making something at 7 PM. The best shops I know keep both capabilities close, because the difference between a 36-hour crisis and a 36-hour deadline is often just the tool you reach for first.
After 11 years of rush orders, I do not believe there is a single 'best' manufacturing process. I believe in delivering certainty. Ultimaker 3D printers like the S5 R2 deliver that certainty when the clock is short and the material is right. CNC machines deliver it when nothing else can hold tolerance or temperature. Pick the route that removes 'maybe' from your schedule—that's the whole skill.