I'm a quality compliance manager at an additive manufacturing services company. Every part that ships from our floor crosses my desk—roughly 1,200 unique parts a year. In 2025, I've already rejected 11% of first articles because the documentation didn't match the physical part. So when I compare an Ultimaker 3 3D printer to CNC machining, I'm not picking brand over process. I'm looking at which one is easier to verify.
From the outside, this looks like a technology comparison. The reality is a quality-planning question: What will you check when the part arrives, and who pays if it's wrong?
Here's the framework I use with my team: material options, dimensional tolerances, inspection workflow, and cost/lead time. Along the way, I'll give a direct answer for each dimension. You may not like all of them.
What Materials Are Suitable for CNC Machining?
Let's answer the keyword question first. CNC machining can work with a wide range of materials: aluminum 6061, steel 4140, stainless 303/304, brass, copper, titanium, Delrin/POM, nylon, PTFE, UHMW, and many composites. If you're searching for CNC machining CT—as in Connecticut—a local shop will usually have stock in aluminum, steel, and common plastics. But stock is not capability. A shop can only cut what it has tooling and feeds/speeds for. Ask for a material list before you design around it.
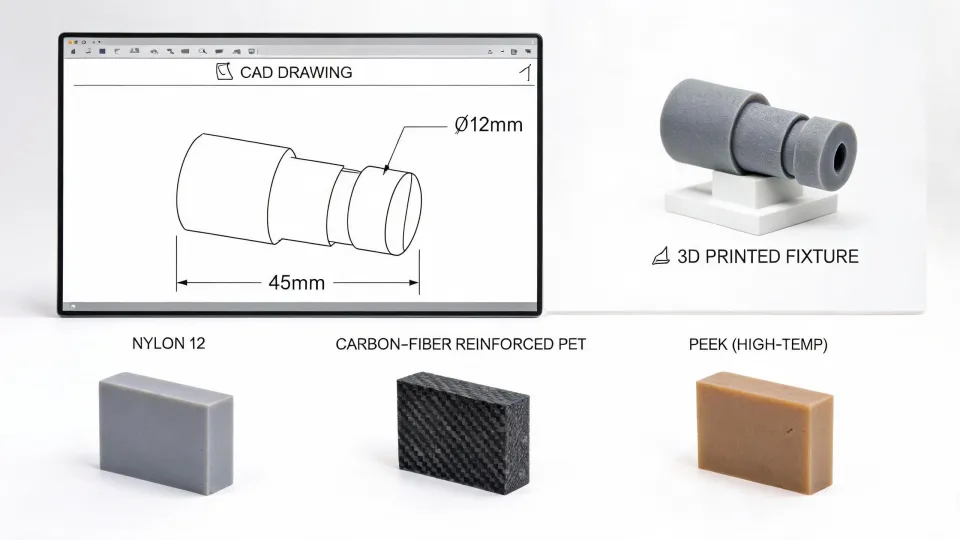
An Ultimaker 3 3D printer, by comparison, is limited to thermoplastics that can be melted and extruded: PLA, Tough PLA, ABS, PETG, TPU, polycarbonate, nylon, and some carbon-fiber or glass-reinforced blends. You cannot print aluminum or steel on it. That's not a flaw in the machine; it's a boundary. I'd rather work with a specialist who knows their limits than a generalist who overpromises.
There's a reason this question keeps coming up: material selection drives the whole quality plan. If you choose a material that isn't actually available, you'll end up with a substituted alloy or a late delivery. I've seen a machinist swap 6061 for 7075 without asking. The part worked, but the material cert didn't match the drawing, and we had to reject it anyway.
The Ultimaker 3 3D printer isn't the newest machine in the lineup now, but it's still a workhorse for dual-extrusion and water-soluble support structures. If your part needs overhangs, a second extruder for PVA makes a huge difference. From a quality standpoint, that means supports can be removed without scarring the part surface.
Tolerances and Surface Finish
For CNC, a standard tolerance is ±0.005 in. (0.13 mm), and many shops can hold ±0.002 in. on critical features. Surface finish routinely reaches 32 Ra. For FDM on an Ultimaker 3 3D printer, layer lines are part of the design. With a 0.2 mm layer height, I use ±0.2 mm as my in-house incoming-inspection threshold for non-critical features. You can improve this with a smaller layer height or post-processing, but it won't become a machined surface.
I once tested a low-run assembly fixture. The CNC version looked beautiful but was too rigid. The printed version absorbed a bit of flex and worked better. That surprised me, because I still expect machined parts to win every functional test. My rule now: measure function, not surface envy.
This was true 10 years ago when FDM was mostly a hobbyist technology. Today, professional FDM is a different animal. But the old belief that '3D printing is always weak' still pushes engineers toward CNC when a printed part would pass the test.
Before you email me asking for exact FDM tolerances, hear this: the right answer depends on geometry. A flat wall on a well-calibrated printer holds tighter than a tall thin tower that moves during printing. In quality inspection, we don't write '±0.2 mm everywhere.' We write 'critical features callout 1-2-3, others reference.' That forces the engineer to think about what actually matters.
How I Inspect Parts From Both Processes
When a CNC part comes in, I check the material certificate against the purchase order, measure critical features with calipers or a CMM, and compare surface finish to the accepted sample. When a 3D printed part comes in, I check the print profile, layer height, infill, and material dryness, then inspect the same critical features. The paperwork is different, but the discipline is the same.
In Q1 2024, we received a batch of 80 CNC-machined brackets where the anodize color was visibly off—Delta E 3.5 against our master sample. Normal tolerance is Delta E < 2 (Pantone Color Matching System guidelines). The vendor claimed it was 'within industry standard.' We rejected the batch, and they redid it at their cost. Now every contract includes a Delta E requirement. For 3D printed parts, the most common rejection reason is not dimensional—it's wrong material or wrong infill. A part can look perfect and fail on the inside.
Digital Factory vs. the Machine Shop Workflow
A CNC machine shop runs on CAM programming, toolpath verification, setup sheets, and in-process inspection. You don't push a button. If you're outsourcing CNC machining in Connecticut, you're managing a supply chain: file transfer, material certs, shipping, inspection reports. It works, but it's a slower rhythm.
For 3D printing, the Ultimaker Digital Factory changes the workflow. As of January 2025, I use it to monitor job status, check which printer is available, and push print profiles from Cura. It's not set-and-forget. (Emphasis on 'not.') But it makes the audit trail easier to follow than a stack of paper travelers from a job shop.
One more thing about the software comparison: Cura profiles matter more than people think. On a CNC machine, speeds and feeds are set by the operator and documented in the setup sheet. In 3D printing, the profile is part of the process spec. When I see a part fail, the first thing I ask for is the Cura profile and the printer's calibration log. Digital Factory gives me that trail. Most outside CNC shops can't share that level of detail about a part from two years ago.
I do not mean 3D printing is better than CNC. I mean the quality plan has to match the process. Digital Factory is easier to verify—assuming the material is dry, the build plate is level, and the profile is correct. Those are big assumptions, but they're visible in the software.
Lead Time, Cost, and Volume
For one-off prototypes, an Ultimaker 3 3D printer usually wins on speed. You can slice, print, and test in a day. CNC machining requires quoting, fixturing, cutting, deburring, and finishing. For 50 to 100 parts, 3D printing is still competitive because there's no tooling. But for 1,000 simple aluminum brackets, CNC machining wins on cost, consistency, and material properties. It's not close.
In my time, teams have bought a professional 3D printer expecting to replace an outside machine shop. That doesn't happen. Additive solves complexity and customization; subtractive solves strength, surface, and volume. They combine well. In our shop, we often print a body and then CNC machine a metal insert for the critical bore.
Pricing differences are harder to generalize. As of January 2025, a small CNC aluminum bracket from a Connecticut job shop will often cost more than the same rough shape printed in PLA, because the CNC order includes setup, programming, and cleanup. But a 3D printed part in polycarbonate can cost more than an aluminum part if it needs multiple attempts and post-processing. The per-part price is the wrong way to compare. The real unit cost includes inspection and risk.
A Boundary Note: CO2 Laser Skin Resurfacing Face
I need to address the keyword outliers. If you landed here from a search for 'co2 laser skin resurfacing face,' please stop. That is a medical/cosmetic procedure, not a manufacturing process. I can review a tolerance on a printed part, but I'm not the person to guide you on skin resurfacing. Call a dermatologist.
And 'cnc machining ct'? If CT means Connecticut, that's a location-specific supplier search. Choose a shop with relevant experience, not a generic online quote. If CT means computed tomography, that's a different engineering field. If you need a 3D-printed model from CT scan data, that's a specialized workflow—send the DICOM data to someone who handles medical segmentation.
The vendor who said 'this isn't our strength—here's who does it better' earned my trust for everything else.
Which Should You Choose?
Here's my direct answer, split by scenario.
- Choose an Ultimaker 3 3D printer when: you need low volume, complex geometry, functional prototypes, custom jigs, or fast iteration. Use the Ultimaker Digital Factory to keep the fleet under control.
- Choose CNC machining when: you need metal end-use parts, tight tolerances, smooth surfaces, high volumes, or material certifications. If your part needs 6061 aluminum or 12L14 steel, the answer is CNC.
- Choose a hybrid workflow when: you can print the geometry that would be expensive to mill, then add machined features for critical fits. This is the quiet secret of good manufacturing engineers.
In my first year, I made the classic specification error: I wrote 'smooth finish' on one drawing and 'good surface' on another. Cost me a $600 redo. Now every contract includes measurable requirements. That lesson applies here too. Don't choose 3D printing or CNC based on hype. Choose based on what you can inspect and defend.
If someone promises one process can handle everything—including laser resurfacing—run. A specialist who knows their limits is more useful than a generalist who overpromises. That's true for 3D printing, CNC machining, and everything in between.