I've been handling manufacturing orders for 12 years. During that time, I've personally made—and documented—14 significant mistakes, totaling roughly $28,000 in wasted budget. Not proud of it, but the silver lining is that our team now uses a checklist I built to prevent others from repeating my errors.
The most frequent question I get isn't "which 3D printer should I buy?" It's a broader one: should we use an Ultimaker 3D printer or traditional manufacturing methods like CNC machining, medical precision laser tube cutting, or press braking? I used to think there was a single right answer. Now I know that's a false binary. The real question is when to use each.
In this comparison, I'll look at three dimensions: design freedom (and DFM in CNC machining), precision and materials, and total cost of ownership. Each one has burned me at least once.
1. Design Freedom vs. DFM in CNC Machining
If you're in the metalworking world, you've likely heard the acronym DFM—Design for Manufacturing. Simply put, DFM means adapting your design to what the machine can actually produce: avoiding sharp internal corners, ensuring tool access, and planning for fixtures. Ignoring DFM in CNC machining was one of my earliest mistakes.
In my first year (2017), I submitted a manifold design with internal channels to a CNC shop. On my screen, it looked perfect. The result came back as scrap—a $3,200 order, straight to the trash. The shop explained that their tools couldn't reach the internal channels without splitting the part in two. That was my first real lesson: CNC is subtractive, so every feature has to be accessible by a cutting tool.
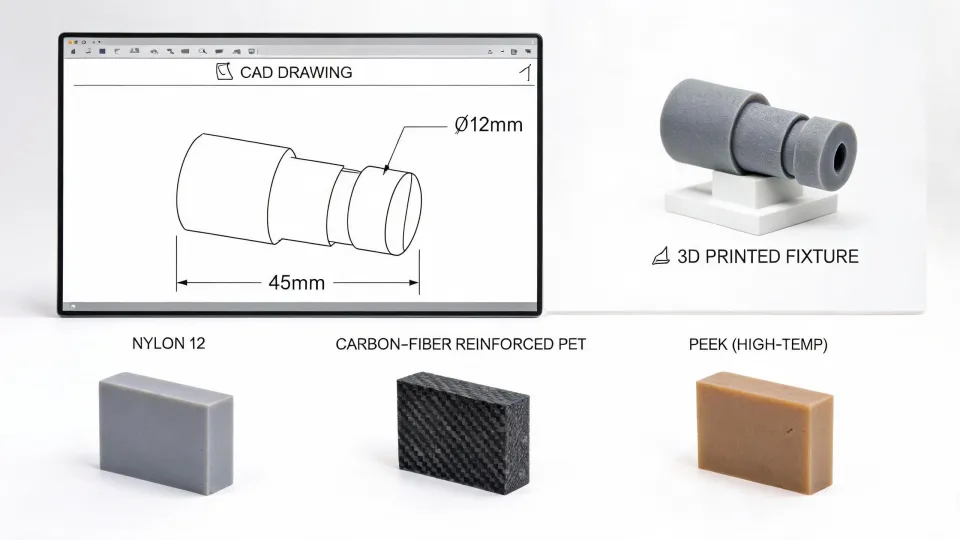
The next year, our shop added a 3D printer Ultimaker 3. I redesigned a similar manifold and printed it in PLA on the Ultimaker 3. No tool access issues, no internal corner limitations—the part came out in one piece overnight. I was hooked.
But here's the counter-intuitive part: that 3D printed prototype worked, but the production cost per part for 500 units was far higher than CNC would have been. The DFM constraints I hated actually existed to keep costs low. Design freedom has a price, and that price grows with batch size. So the lesson wasn't "3D printing replaces CNC." It was "use 3D printing for complex geometry and low quantities, and CNC for simpler parts and higher volumes."
When people ask me what is DFM in CNC machining, I give them a concise answer: it's a reality check for your CAD model. It asks: can this part actually be made with the available tools, and at what cost? 3D printing bypasses many of those constraints, but you pay for the luxury in unit cost.
2. Precision and Materials: Ultimaker vs. Medical Precision Laser Tube Cutting
The dimension that most often trips up engineers is precision and material properties. I learned this while working with a medical device client who needed a titanium stent fixture.
The spec called for medical precision laser tube cutting—a process that cuts thin-wall metal tubes with tolerances around ±0.05 mm, leaving a clean, minimally heat-affected edge. I wanted to impress the client by showing off our new Ultimaker S5. But honesty forced a concession: FDM 3D printing can't cut metal, and a 0.2 mm layer line isn't in the same league as a laser-turned edge.
That said, we did find a place for 3D printing in the same project. (Should mention: we printed patient-specific surgical guides in medical-grade resin—but that's a different printer, not FDM.) For pre-surgical planning, we printed an anatomical model of the patient's artery from CT scan data. The laser cutting company looked at that model and said it helped them plan the tube lengths more accurately than 2D drawings. So they weren't enemies; they were complementary.
Honestly, I'm not sure why some vendors quote extremely tight tolerances without stating the inspection method. My best guess is they measure only the first article and assume the rest are identical. So we added a step to our checklist: confirm the Cpk or at least get a run chart. That simple addition has caught 12 potential tolerance failures in the past 18 months.
3. Efficiency and Batch Size: Hogi Press Brake vs. 3D Printing
If you're wondering where a press brake fits in a 3D printing discussion, let me give you a real scenario. A Hogi press brake is a traditional sheet metal bending machine. For brackets in quantities of 1,000+, a skilled operator can produce dozens per hour. I've seen a Hogi press brake make more brackets in one shift than my Ultimaker could make in a month. It's brutally efficient.
But here's where the binary thinking fails: setup time. For a one-off bracket, the press brake needs tooling changes, trial bends, and inspection. That workflow took two full days in September 2022. Meanwhile, the Ultimaker printed the same bracket (in PLA, not metal) in two hours. The design wasn't final, so those two hours bought us a week of iteration.
Switching to a more efficient hybrid workflow—3D printing for prototypes, press brake for production—cut our turnaround from 5 days to 2 days. The automated process also eliminated the data-entry errors we used to have when manually recalculating bend allowances. That efficiency gain wasn't just about cost; it gave our engineers more time to think.
That said, I get why shops are slow to adopt 3D printing. Press brakes and CNC machines are reliable workhorses, and their cost per part is predictable. But if your bottleneck is iteration speed, additive wins for small quantities.
I went back and forth between buying a second Ultimaker and outsourcing our prototypes to a machining job shop for two weeks. On paper, outsourcing made sense: I didn't have to train anyone. But my gut said we'd lose control of the iteration loop. Ultimately, I chose the second Ultimaker because our design cycle was the bottleneck. That decision still gives me doubts occasionally—especially when I look at maintenance costs—but it has paid off in faster time-to-prototype.
4. Total Cost of Ownership (The $28,000 Math)
The cheapest per-part quote can be the most expensive decision you make. In June 2020, I approved a $4,800 order for laser-cut steel spacers because the per-unit cost was 30% lower than the 3D printed version. But the laser vendor missed the deadline by five days due to material rework. That delay cost us a client relationship worth roughly $12,000.
I'm not saying 3D printing would have been better—the part required metal, and metal is not an FDM material. The real mistake was optimizing on unit price instead of total cost of ownership.
Here's the math I use now:
- Total cost = base product price + setup fees + shipping + rush fees + potential rework costs + delay costs
- If the design is still changing → 3D printing (low iteration cost)
- If the quantity is under 100 → 3D printing (no tooling)
- If the material must be metal, isotropic, or match a rigid spec → traditional (CNC, laser cutting, press brake)
- If the supplier's reputation is uncertain → choose the more certain path, even at a higher price
Also, don't believe anyone who promises 100% print success.
Per FTC guidelines (ftc.gov), claims must be truthful and substantiated.A vendor who says "guaranteed first-try prints" is probably not measuring failures. Our first-year failure rate on the Ultimaker was around 15%—mostly due to bad bed adhesion on the Ultimaker 3. Once we added a routine bed-level check, that dropped to 4%.
Choosing Sides: My Practical Advice
If you're making medical implants or high-precision metal components, medical precision laser tube cutting or 5-axis CNC is your starting point—not an Ultimaker. If you're prototyping, customizing, or producing small batches of complex plastic parts, an Ultimaker (S3, S5, S7, or Factor 4) with Cura software is hard to beat. If you're looking for the Ultimaker download, it's the software page for Cura—free and worth every penny. If you're bending sheet metal in high volume, a Hogi press brake will be your workhorse. Just don't try to force it to make complex internal geometry.
The most efficient organizations are hybrid—they let each method do what it does best. The ones that fail become ideological about a method. Don't be that person.
Even after 12 years, I second-guess some of my early decisions. But the checklist helps. Since we implemented it in Q1 2024, we've caught 47 potential errors in 18 months. That's roughly $47,000 in avoided rework—or rather, 47 headaches avoided.
Hope this saves you a few of the mistakes I made.